Guides
What a wrap and tint shop inspection protocol should catch
A wrap and tint shop quality inspection protocol: the order to look in, the light to look under, and the defects that only appear weeks after collection.
What to take away
- Inspect in a fixed order3 feet, then 12 inches, then a raking light at 45 degrees.
- The film maker's post-heat temperature and hold time is a check item, not a guess.
- The failures that matter appear weeks later at edges and recesses, so the follow-up visit is the real test.
- Log one line per finding and read the log monthly. That turns inspection into a process change.
Why a fixed order beats a general look
Two people looking at the same wrap find different things. The same person finds different things on a Friday afternoon.
A fixed order, a set light position and two measured distances make inspections comparable. Findings become reportable. "Lifted at the rear edge of the driver door recess" is actionable. "Looks a bit rough" is not.
General vehicle inspections follow the same principle: a defined sequence with known failure points catches more than experience alone. Bay lighting and the lamp itself are covered in the shop equipment and setup guide, worth reading before buying a light that flatters film instead of revealing it.
The protocol
Run this indoors on a clean vehicle, before the customer sees it. Direct sun hides the defects you are looking for. Same order, every vehicle, every inspector.
Inspection Protocol Order
- Walk at three paces for panel problems
- Walk at arm's length for edges
- Rake light across flat panels
- Open doors, check jambs and terminations
- Check recesses by touch and eye
- View glass from inside and outside
- Confirm hardware refitted and tight
- Photograph in fixed positions
- Wash, dry and pull the vehicle inside. Mixed daylight and overhead lamps flatten the surface you have to read.
- Walk the full perimeter at about 3 feet (1 m). Look for panel alignment and color match only.
- Repeat the walk at 12 inches (30 cm). At this distance read contamination specks, seams and edge roll-back.
- Set the raking light. Hold a handheld LED bar at roughly 45 degrees to the panel and sweep it slowly across each one.
- Take surface temperature against the film maker's post-heat specification. Most publish a surface temperature and a hold time per product line. A vehicle released early is a scheduling failure, and the scheduling guide treats those with buffers rather than optimism.
- Inspect edges and recesses last. Door edges, wheel arches and mirror bases get the same pass.
- Check the glass. Read the dot matrix band, the defroster lines and the edge gap at each moving window.
- Photograph a fixed shot list against the job number. Same angles, same light, every vehicle.
What the defect table catches
| What you see | What it usually means | When it shows up |
|---|---|---|
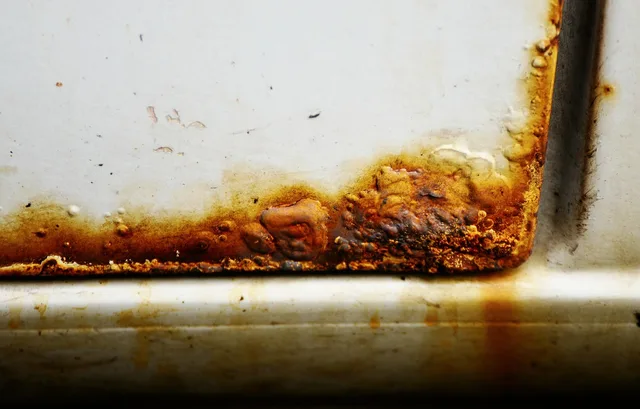
| Lifting at a recess or deep edge | Film was not post-heated to the maker's specification | Weeks to months after collection |
| A speck or raised point under the film | Contamination on the panel or in the air | Immediately, under raking light |
| A silvered or hazy band at the top of glass | Film against the dot matrix band, a known material limit | Immediately, and it should have been disclosed at quoting |
| Small water pockets and haze on new tint | Normal drying over the stated period | On collection, clearing afterwards |
| A visible seam where none was planned | A panel needed more than one piece, joined poorly | Immediately |
| Color difference between fleet vehicles | Panels printed on different runs or lots | When two vehicles park side by side |
| Adhesive residue after removal | Removal cut short, or old film needing more heat | On collection |
| An edge cut on paint | A blade where knifeless tape belonged | Immediately, and it is a paint repair |
Defect, Cause, Timing
What you see
- Lifting at recess
- Not post-heated
- Speck under film
- Contamination
- Silvered dot matrix band
- Material limit
- Water pockets on tint
- Normal drying
- Visible seam
- Poor join placement
- Fleet color difference
- Different print runs
- Adhesive residue
- Removal cut short
- Edge cut on paint
- Blade not tape
What it means
- Lifting at recess
- Weeks to months
- Speck under film
- Immediately
- Silvered dot matrix band
- Immediately
- Water pockets on tint
- Clears after
- Visible seam
- Immediately
- Fleet color difference
- Side by side
- Adhesive residue
- On collection
- Edge cut on paint
- Immediately
When it shows
- Lifting at recess
- Speck under film
- Silvered dot matrix band
- Water pockets on tint
- Visible seam
- Fleet color difference
- Adhesive residue
- Edge cut on paint
The first row defines this trade. Lifting at a recess is invisible on collection day and is the standard long-term failure. The follow-up below matters more than the final inspection.
The follow-up visit nobody schedules
Pick a rolling sample of completed vehicles and look at them again several weeks later. Ask the customer to bring the vehicle back, or photograph it when it returns.
Read two things only: edges and recesses. If they are down, your preparation and post-heat are sound. If they are lifting, the fault is upstream and every vehicle delivered since carries it.
The intake-to-collection flow is mapped in the operations and workflow guide, the right next read if findings keep clustering at one stage.
A wrap that lifts at a recess three weeks after collection was released too early or stretched too far. Both causes sit upstream of the inspector.
Turning findings into a short defect log
Keep one line per finding: vehicle, job number, what was found, the stage that should have caught it, and what changed. Read it monthly and look for one stage repeating.
Findings that cluster at preparation point to discipline. Findings at application point to training or the environment. Findings at release point to timing against the hold period.
The IRS guidance on records a business should keep describes documents supporting what happened. Photographs filed against a job number answer a complaint two years later.
Safety and waste around the inspection
Crawling under a van or reaching a roof is a hazard in its own right. OSHA's safety management guidance is built on finding and fixing those hazards before an injury does. Give the inspector safe access.
Rework also creates waste, so catch the defect before the film goes on. The daily discipline that keeps findings low, and rework rare, is written up in the SOP checklist for daily operations.